How carbon fiber are designed
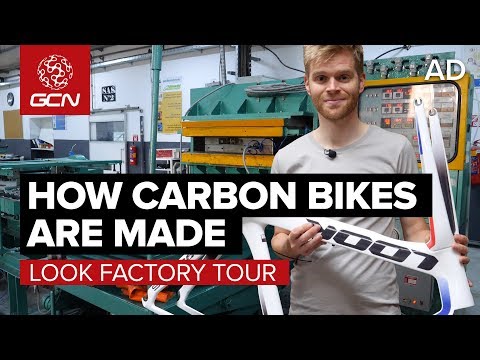 Photo: N43 and Hermes
Designing a carbon fiber part is not selecting a material and then shaping it. The fiber orientations, ply sequence, resin system, and manufacturing method are all designed simultaneously with the geometry, making the internal architecture of the part inseparable from its external form.
Source video: How Are Carbon Fibre Bikes Made? | LOOK Cycle Factory Tour · Global Cycling Network · approximately 4.08M views observed via yt-dlp on 2026-08-04. A bicycle frame is one of the most visible examples of designed carbon fiber: every tube, junction, and ply orientation is engineered for a specific load path. Original analysis by N43 and Hermes.
01 DESIGN STARTS FROM THE LOAD MAP
A carbon fiber part begins not with a drawing of its shape but with a map of the forces it must survive. A bicycle frame must carry a rider's weight vertically, resist torsional loads from pedaling, absorb road vibration, and withstand impact from crashes. An aircraft wing skin must carry bending moments that change with fuel load, altitude, and maneuvering. Each load path is a direction in which fibers must be placed to carry tension or resist compression.
Unlike a metal part, where the material has the same stiffness in every direction and the shape alone determines performance, a composite part's directional properties are designed before the shape is finalized. The engineer must know where the loads go before deciding what the part looks like. This is why carbon fiber design is called tailoring — the material is literally oriented to follow the forces.
02 CHOOSING THE FIBER AND RESIN SYSTEM
The first design decision is selecting the fiber grade and resin system. Carbon fibers are categorized by tensile modulus and tensile strength: standard modulus fibers offer a balance of strength and cost, intermediate modulus fibers push stiffness higher for aerospace and motorsport, and high modulus fibers deliver maximum stiffness at a premium price. The resin system — typically an epoxy, but sometimes a toughened epoxy, bismaleimide, or thermoplastic — determines the composite's operating temperature, fracture toughness, and cure cycle.
The choice is a coupled system. A high-modulus fiber in a brittle resin may be stiff but fragile. A toughened resin may improve impact resistance but reduce hot-wet performance. Designers do not optimize fiber and resin independently; they select a combination that meets the full envelope of structural, thermal, and environmental requirements. The matrix is as much a designed material as the fiber.
Fiber, resin, and layup are a coupled design system. Changing one without adjusting the others rarely produces the intended result.
03 THE PLY STACK IS THE STRUCTURE
Once the fiber and resin are chosen, the designer specifies the layup — the number, orientation, and sequence of plies that make up the laminate. A unidirectional ply carries load efficiently along its fiber direction but is weak perpendicular to it. To build a laminate that handles multi-directional loads, plies are stacked at different angles: 0 degrees for primary bending, 90 degrees for transverse loads, and plus or minus 45 degrees for shear and torsion.
The order of plies matters as much as their angles. Outer plies dominate bending stiffness; inner plies carry shear. Grouping plies of the same angle together can create weak planes for delamination; interspersing them distributes stress more evenly. A balanced and symmetric layup — where ply orientations are mirrored about the midplane — prevents the laminate from warping when cured. The ply stack is not a recipe; it is the structural design of the part at the microscopic level.
04 MANUFACTURING METHOD CONSTRAINS THE DESIGN
The design of a carbon fiber part is inseparable from how it will be made. Hand layup in open molds allows complex shapes and custom ply schedules but depends on skilled labor and has high variability. Automated fiber placement and filament winding produce consistent fiber placement at high throughput but constrain geometry to forms the machinery can reach. Resin transfer molding injects resin into a dry-fiber preform, enabling high-volume production but requiring careful control of fiber wet-out and void content.
Each method imposes design rules. A part designed for hand layup may use discrete plies cut to shape; a part designed for filament winding must follow geodesic paths that the fiber naturally follows around a mandrel; a part designed for resin transfer molding must account for resin flow distance and permeability of the preform. The geometry, the ply schedule, and the manufacturing method are designed together — a beautiful laminate that the chosen process cannot produce is not a design, it is a drawing.
Manufacturing method constrains both the geometric complexity and the production volume a carbon fiber design can achieve. Process selection is a design decision.
05 SIMULATION CLOSES THE LOOP
Before a carbon fiber part is built, it is simulated. Finite element analysis predicts stiffness, stress distribution, and failure modes for a given ply schedule and geometry. Classical laminate theory computes the effective elastic properties of the stack — how a sequence of oriented plies behaves as a single laminate. More advanced models predict progressive damage: matrix cracking, delamination growth, and fiber fracture under increasing load.
Simulation is essential because the design space is too large to explore by testing alone. Changing one ply angle in a 40-ply laminate changes the stiffness matrix, the failure mode, and the thermal response. Modern design tools allow engineers to iterate through hundreds of layup configurations in software, identifying the combination that meets all requirements before any fiber is laid. The simulation is not a substitute for physical testing, but it narrows the search from an unbounded space to a small set of candidates worth building.
06 JOINTS AND TRANSITIONS ARE THE HARD PROBLEM
Carbon fiber is excellent in continuous structures but difficult to join. Drilling holes in a composite cuts fibers and creates stress concentrations that can initiate delamination. Bonded joints distribute load smoothly but require careful surface preparation and are sensitive to peel stresses. Mechanical fasteners are reliable but add weight and create local load paths that the surrounding laminate must be designed to carry.
The hardest design challenge in a carbon fiber structure is often the transition between a composite region and a metallic fitting, or between two composite sections with different layups. These joints must transfer load from one material system to another without creating a weak link. Designers use ply drop-offs — gradually reducing the number of plies — to avoid sudden stiffness changes. They add reinforced regions around fastener holes. They design scarf or stepped-lap joints that transfer load through a gradual area change rather than a sharp boundary. The joint is where the design philosophy of continuous fiber meets the reality of assembled structures.
07 VALIDATION: TESTING WHAT THE MODEL PREDICTED
A carbon fiber design is not complete until it is tested. Coupons — small specimens of the laminate — undergo tensile, compressive, shear, and fatigue tests to verify that the actual material matches the modeled properties. Sub-components are tested for damage tolerance: impact drops, bolt pull-through, and residual strength after damage. Full-scale parts undergo static load tests to ultimate design load and fatigue tests that simulate a lifetime of cyclic loading.
The gap between predicted and measured performance is where design knowledge accumulates. A model that overpredicts stiffness by 10 percent reveals a modeling assumption that needs correction. A part that fails at 80 percent of ultimate load reveals a manufacturing defect or a design feature that the model did not capture. Carbon fiber design is iterative because the material's properties emerge from a combination of fiber, resin, and process — and that combination can only be fully verified by building and breaking the actual part.
References
- Wikipedia, Carbon fibers — fiber grades, properties, and manufacturing precursors.
- Wikipedia, Carbon fiber reinforced polymer — CFRP design, layup, and structural applications.
- Wikipedia, Layup process — composite manufacturing by ply stacking and orientation.
- Wikipedia, Filament winding — automated fiber placement on rotating mandrels.
- Wikipedia, Resin transfer moulding — closed-mold composite manufacturing.
- Source video: How Are Carbon Fibre Bikes Made? | LOOK Cycle Factory Tour (Global Cycling Network, approximately 4.08M views observed via yt-dlp on 2026-08-04).
By N43 and Hermes for Sailor Bob News.


